How to Make Your Diamond Saw Blade Last Longer | GUSHI
Most diamond blades don't wear out. They get killed — by heat, by a dirty flange, or by being the wrong disc for the material. Fix those three and you'll get more cuts per blade. How many more depends on what you're cutting and who's running the machine, and anyone who quotes you a fixed number hasn't seen your site.
Start at the flange
Before you look at the diamond, look at the flange. A chip of dried slurry, a burr, a bit of grit — anything under there tilts the blade and puts the stress on one side of the core. You won't notice it in the first cut. You'll notice it later, as a crescent worn into one side of the rim.
Tighten it to the figure on the blade or in the machine manual. Not the impact gun, and not "two grunts and a half". Too loose and the blade slips on the arbor and burns. Too tight and you dish the flange, which is the same problem you were trying to avoid.
Check the arrow. It sounds obvious until you've watched a blade run backwards for a week.
On a wet saw, water has to hit both sides of the rim. One side only and you get a temperature gradient across the segment — one side wears, the other glazes.
Where blades quietly go bad
Storage kills more blades than cutting does. Standing one against a damp wall, or laying it flat on a concrete floor, is how you get a rust ring on the core. Hang it, or stand it on edge somewhere dry. If it's going to sit for months, wipe the core with a thin oil and wrap it. Don't stack them so one blade's segments are pressing into the next.
Water is the other quiet one. Not the water itself — the flow. A kinked hose, a half-clogged nozzle, a tray full of grey sludge: the blade is still turning, still cutting, and cooking. Keep both nozzles open and the water clean. If your tray is furring up with scale, that scale is going onto the blade too.
The rim tells you what happened
You can read the last few weeks of work off the rim.
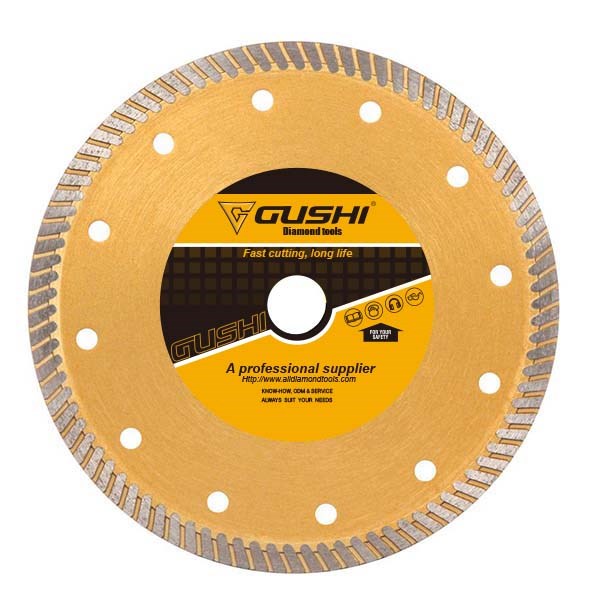
Glazed? Dress it once, then decide
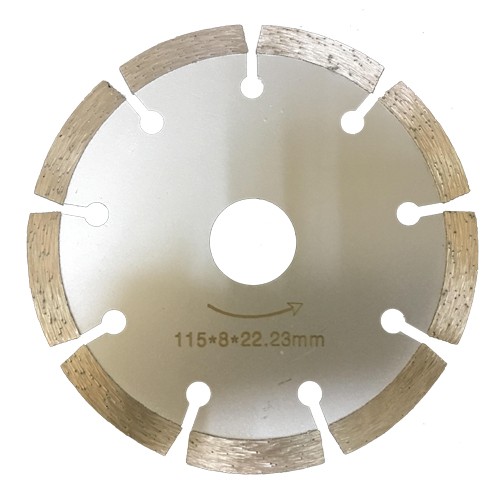
A glazed blade looks fine. The rim is shiny, the segments are all there, and it won't cut. That's not a worn-out blade — the diamond is still in there, it's just buried under smeared metal.
Run a silicon carbide dressing stick lightly against the rim while it turns, or take a few short passes in a dressing block. Light pressure. You're trying to open the surface, not grind the segment down.
If it comes back, good. If it glazes again in the same shift, something else is wrong — wrong blade, no water, or too much pressure. Dressing it a third time is just burning time. And if the segment is already close to the core, don't dress it at all. Replace it.
When to stop
Stop when the segment is close to the steel core. A segment that lets go at cutting speed doesn't care what the blade cost. Stop if the core is cracked, bent, or showing fatigue lines. Stop if it still vibrates after dressing with clean flanges. Stop if a segment is loose or missing.
The last one sounds obvious. It still happens, usually on a Friday, usually to finish a job.
Keep a note
Not a spreadsheet — a note on the wall is enough. Date, material, roughly how many hours, when you dressed it. After five or six blades you'll know your own interval. It won't match the next shop's, and it shouldn't; they're cutting different stone with a different hand.
What doesn't work
Additives. "Break-in" rituals. Running a tile blade through metal because it's the one already on the machine. Leaning on the feed because the blade feels slow.
More pressure doesn't cut faster. It makes heat, and heat is what takes the diamond out of the bond. If a blade is slow, it's usually glazed, or it's the wrong blade, or the water isn't getting where it needs to go.
We sell blades, so take this however you like. But the ones that come back as complaints are almost never worn evenly. They're glazed, cracked, or they were run dry.
Frequently asked
How much longer will my blade last if I do this?
It depends on the material and the operator. There's no fixed number — but fixing heat, blade choice and flange condition is what moves it.
How can I tell if a blade is glazed?
The rim goes shiny and the cut goes quiet; the blade starts to skate instead of bite. The segments are still there, the diamond is just buried.
Is dry cutting always wrong?
No. Some blades and materials are rated dry. Check the marking on the blade — if it's a wet blade, run it wet.
Dress it or replace it?
Dress it if the segment still has height and the core is sound. Replace it if the segment is near the core, the core is cracked or bent, or it glazes again straight after dressing.
Does hard water matter?
It leaves scale, and scale cuts down cooling. If your tray is furring up, filter or soften the water.